
Reading Radiographic Reports: AST vs GB RT Grades for Castings
Publication Date : 2026-10-19 03:10:34
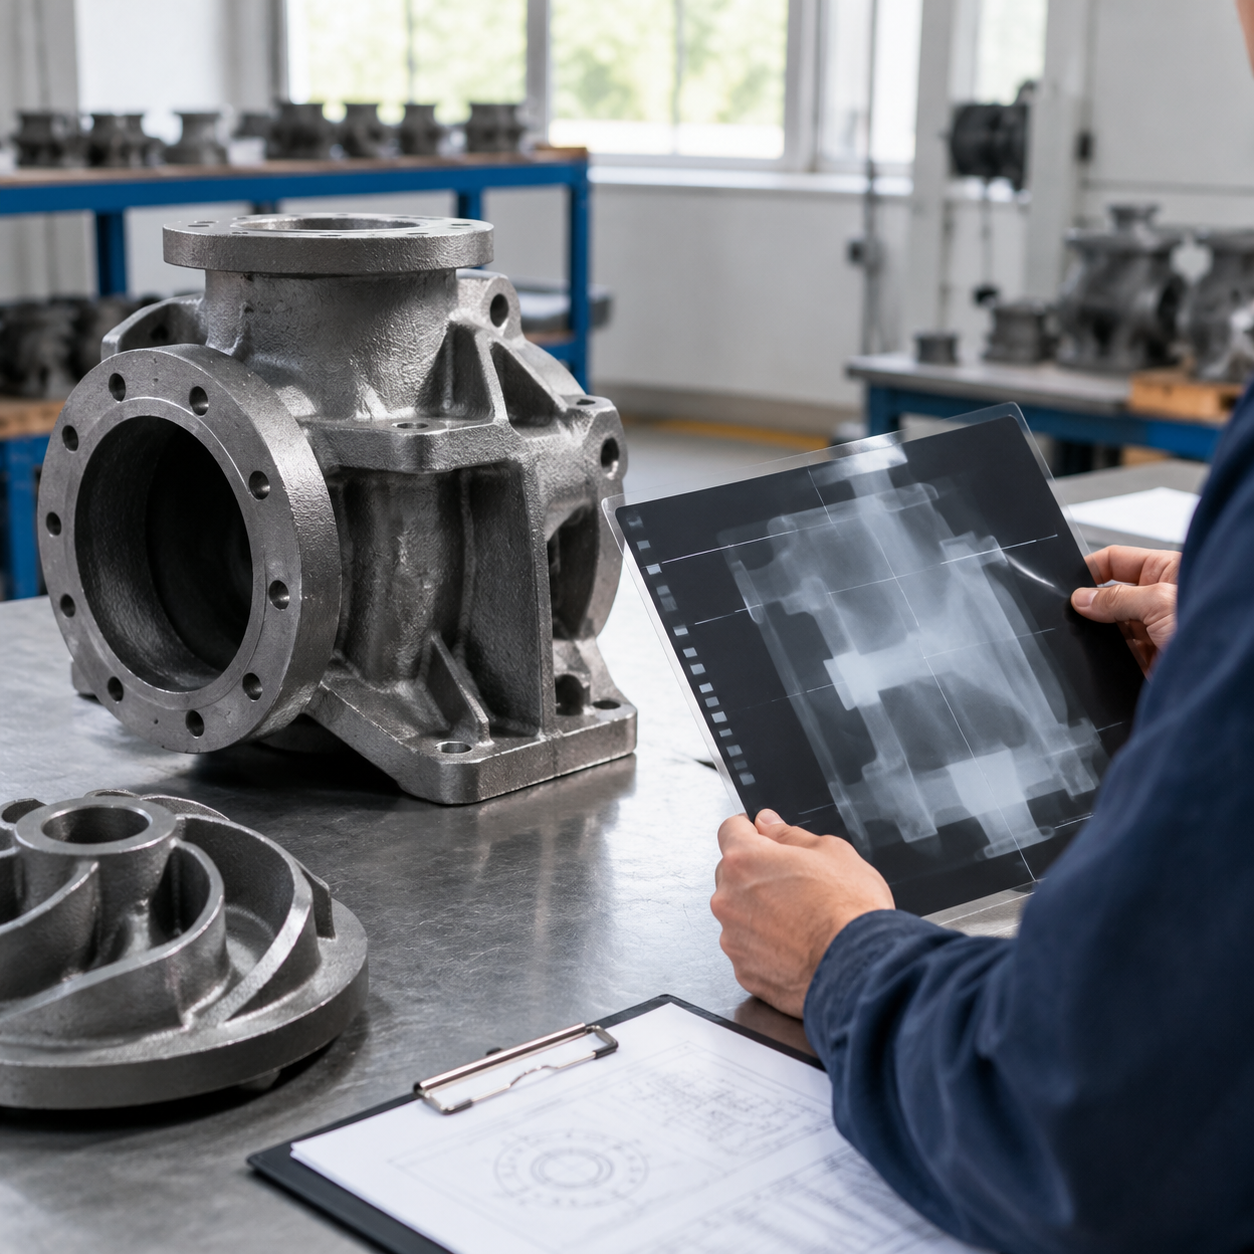
A practical guide for overseas buyers on how ASTM E446/E505/E186 and Chinese GB/T radiographic grade systems map to acceptance levels, how the grade numbers differ between standards, and exactly what to write on a casting drawing so the foundry and the RT lab interpret your requirement the same way.
Why the Grade Number Alone Is Not Enough
A radiographic report that says "Grade 2 accepted" tells you almost nothing until you know which standard produced that number. ASTM E446 (steel castings up to 2 in. / 51 mm), E186 (heavy-wall steel, 2–4.5 in. / 51–114 mm), and E505 (aluminum and magnesium) define severity levels by reference radiographs, and the level is tied to a specific discontinuity type—gas porosity, sand inclusion, shrinkage, or crack. GB/T 5677 (steel) and GB/T 9438 (aluminum) use a parallel but not identical numbering scheme. A Chinese foundry quoting "Grade 2 per GB" and a US buyer expecting "Grade 2 per E446" may be talking about different acceptance thresholds, especially for shrinkage and inclusion categories.
The fix is procedural, not technical: specify the standard, the severity level, the discontinuity category, the wall thickness range the level applies to, and the acceptance class for each zone of the casting. Do that on the drawing and in the purchase order, and the RT report becomes verifiable rather than negotiable.
How the Grade Levels Map to Acceptance
In practice, most structural and pressure-adjacent castings are specified between Grade 1 and Grade 3. Grade 1 is the tightest: only minimal, scattered indications are permitted, and it is normally reserved for critical sections, sealing surfaces, or fatigue-loaded areas. Grade 2 is the common commercial baseline for machined surfaces and load-bearing sections. Grade 3 and above accept progressively larger and denser indications and are usually limited to non-critical, thick, or as-cast surfaces. The chart below shows a typical distribution of specified grades across a mixed order of steel and aluminum castings—useful as a sanity check when a foundry proposes a grade far from the norm for your part type.
Two practical cautions. First, severity levels are thickness-dependent: the same Grade 2 allows larger indications in a 100 mm section than in a 20 mm section, so a drawing that does not state the thickness range is ambiguous. Second, acceptance is per discontinuity type—a casting can pass Grade 2 for porosity and fail Grade 2 for shrinkage in the same radiograph. Always require the report to list each category separately.
Reading the Report: What to Check Line by Line
A usable RT report contains the standard and revision year, the severity level per discontinuity type, the technique (X-ray or gamma source, film or digital), the source-to-object distance, the IQI (image quality indicator) sensitivity achieved, the wall thickness at each shot, and a disposition (accept/reject/repair). If any of these is missing, the report cannot be audited against the drawing. Ask for the IQI sensitivity value in particular: a report that claims Grade 2 but was shot at 4% sensitivity may not be capable of resolving the indications that grade requires.
Compare the report's stated thickness against the drawing's section thickness. A common failure mode is RT performed on a thicker boss or riser contact area and then applied to the whole casting. Also confirm that repair welds were re-radiographed to the same grade, not to a looser one.
- Standard and revision year (e.g., ASTM E446-20 or GB/T 5677-2018)
- Severity level stated separately for porosity, inclusion, shrinkage, and crack
- Radiation source and film/digital technique
- Source-to-object distance and focal spot size
- IQI sensitivity achieved (%) and IQI location
- Wall thickness at each radiographed area
- Disposition per area, with repair and re-test records
What to Write on the Drawing
Put the RT requirement in a dedicated note block, not buried in general tolerances. State the standard, the grade per discontinuity type, the zones to which each grade applies, and the thickness range. If different areas need different grades—say Grade 1 on a sealing face and Grade 3 elsewhere—mark those zones on the drawing with a clear boundary. Specify the extent of radiography (100% of critical zones, or a stated sampling percentage for others) and the stage at which it is performed (after heat treatment, before machining).
The chart below compares the acceptance strictness implied by common grade specifications across standards, normalized to a 0–100 scale where 100 is the tightest acceptance. It is a planning aid for aligning ASTM and GB requirements, not a substitute for the standard text. When in doubt, attach the reference radiograph plates or a written acceptance table to the PO so both sides work from the same picture.
Aligning ASTM and GB Requirements in a Purchase Order
When a buyer's drawing cites ASTM and the foundry works to GB, the cleanest approach is a one-page RT annex to the PO: it lists the standard pair, the equivalence table you have agreed (grade by grade, category by category), the thickness bands, and the disposition rules for each. Have the foundry's RT lab sign it. This removes the ambiguity that otherwise surfaces only when a report is disputed.
Finally, budget for the practical cost of tighter grades. Moving from Grade 3 to Grade 2 typically increases RT film/digital volume and may trigger rework on shrinkage-prone sections; moving to Grade 1 can materially change yield and price. Specify the loosest grade that satisfies the service condition, zone it, and document it. That is cheaper than arguing about a report after the castings are on the water.
Frequently Asked Questions
Is ASTM E446 Grade 2 equivalent to GB/T 5677 Grade 2?
Not automatically. The two standards use similar severity concepts but different reference radiographs and thickness bands. Treat them as comparable, not identical, and agree a written grade-by-grade mapping in the PO annex before production. For critical sections, attach the reference plates or an acceptance table.
Which grade should I specify for a machined sealing surface?
Grade 1 for the sealing zone, with a clearly marked boundary on the drawing, and Grade 2 or 3 for the rest of the casting. State the thickness range and the discontinuity categories covered. Specifying Grade 1 across the whole part unnecessarily raises cost and rework risk.
What must an RT report include to be acceptable?
The standard and revision year, severity level per discontinuity type, technique and source, source-to-object distance, IQI sensitivity, wall thickness per shot, and a clear disposition with repair and re-test records. A report missing the IQI sensitivity or the thickness cannot be verified against the drawing.
Looking for a reliable casting supplier? Request a quote from Intercontinental Casting — our engineering team replies within one business day.