
How to Read a CMM Inspection Report for Castings
Publication Date : 2026-10-21 03:10:38
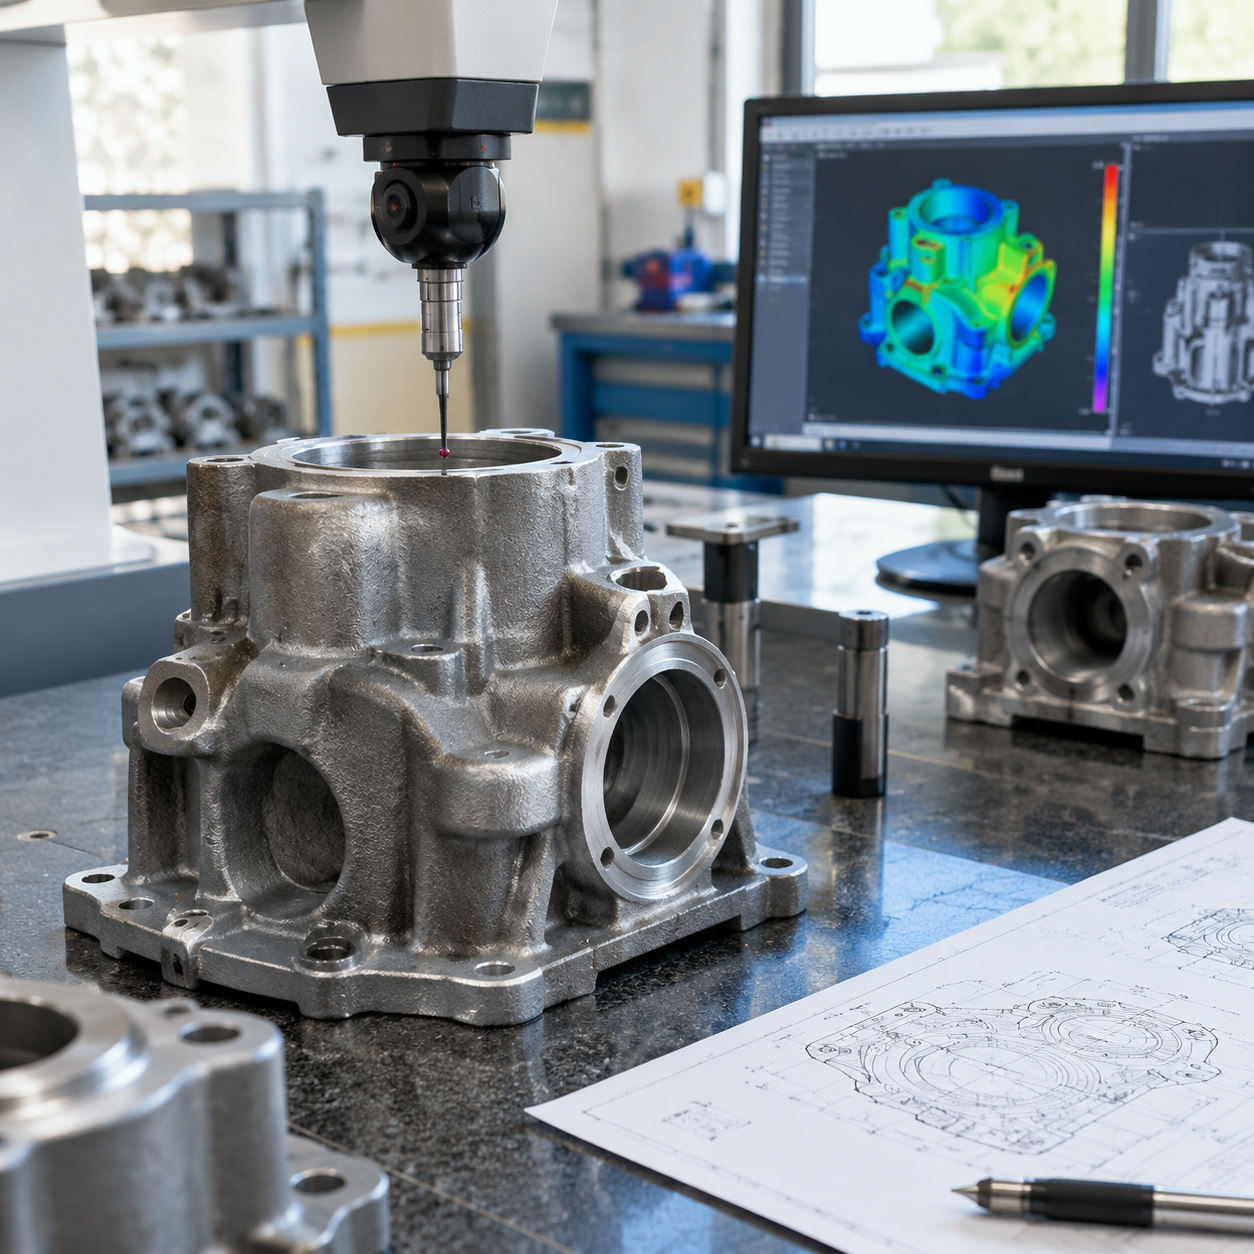
A CMM report is only as good as the datum scheme and GD&T callouts behind it. This guide shows casting buyers how to verify datum alignment, interpret position and profile tolerances on as-cast surfaces, and catch the most common reporting traps before they turn into a rejected lot.
Start With the Datum Scheme, Not the Numbers
Before you look at a single measured value, find the datum reference frame at the top of the report. A coordinate measuring machine reports every dimension relative to the datums it was aligned to, so if the setup does not match the drawing, every number downstream is suspect. Check that the primary datum is the one the drawing calls out (usually the largest machined face or the mounting plane), the secondary is a feature that constrains rotation, and the tertiary locks the remaining degree of freedom. On castings, the primary datum is often a machined pad, while secondary and tertiary datums may be as-cast surfaces or two bored holes.
A common failure is datum shift between the foundry and the machine shop. If the foundry's CMM aligns to raw casting surfaces and the machine shop aligns to the finished machined face, the same part can show flatness differences of 0.2–0.5 mm depending on which surface is used. Ask the supplier to state the datum targets and the number of points used to establish each datum plane. A plane built from three points on a rough as-cast surface is far less repeatable than one built from 15–20 points on a machined face; a reasonable minimum for a machined datum is 9–12 points spread across the surface area.
Also confirm the report states the alignment method: best-fit, datum-only, or constrained. A best-fit alignment can hide a warped casting by splitting the error across all features, making a 0.8 mm bow look like 0.3 mm. Datum-only alignment is what you want for acceptance decisions.
Reading GD&T Callouts on As-Cast Surfaces
GD&T on castings splits into two families: tolerances that control location and orientation of machined features (position, perpendicularity, concentricity) and tolerances that control the as-cast skin (profile of a surface, flatness, wall thickness). For a position tolerance like ⌖ 0.3 Ⓜ A B C on a bolt hole, the reported value should be the diametrical deviation of the hole axis from true position, and the bonus tolerance from the maximum material condition (MMC) modifier must be shown separately. If the report shows only a single 'position' number without the bonus calculation, ask for the raw axis coordinates so you can verify it.
Profile of a surface is where most disputes start. A callout of ⌓ 0.8 on a cast surface means the entire surface must lie within a 0.8 mm band centered on the nominal CAD surface, so the reported value should be the total band width (max deviation minus min deviation), not the largest single point. A report that lists only a maximum deviation of 0.4 mm under a 0.8 mm profile tolerance is incomplete; the true band could be 0.9 mm once the opposite side of the surface is measured. On sand castings, expect profile deviations of 0.5–1.5 mm on non-critical surfaces and 0.3–0.6 mm on surfaces that will be machined; die castings typically hold 0.15–0.4 mm.
Watch for tolerances applied to features that cannot be measured as drawn. A perpendicularity callout to a datum that is itself an as-cast surface with 1 mm of draft is nearly meaningless without a note on where the datum is established. Ask the supplier to document any deviation from the drawing's datum scheme in the report header.
Common Report Traps and a Pre-Acceptance Checklist
The most expensive trap is a report that passes every characteristic while the part does not fit. This usually means the CMM measured a cleaned, fixtured, temperature-soaked sample rather than production parts, or the report covers only one cavity from a multi-cavity tool. Check the report header for part serial numbers, cavity numbers, inspection temperature (20 ± 2 °C is standard), and the CMM's calibration status. A report without traceable serial numbers cannot support an acceptance decision on a lot.
Second, look at the measurement uncertainty statement. If a feature's tolerance is 0.2 mm and the stated uncertainty is 0.05 mm, the part is effectively being judged with a 25% uncertainty band; that is acceptable only if the supplier applies guard banding (accepting only parts inside 80–90% of the tolerance). Third, verify that the report distinguishes between 'measured' and 'reported' values: some software rounds to two decimals, which can turn a 0.304 mm position into 0.30 mm and mask a marginal failure.
Finally, compare the report's feature list against the drawing's ballooned characteristics. A casting drawing with 40 ballooned dimensions should produce a report with 40 line items plus the datum setup; anything fewer means characteristics were skipped. Request the raw point cloud or DMIS output for any characteristic within 20% of its tolerance limit.
- Confirm datum targets and alignment method (datum-only, not best-fit) are stated in the report header
- Verify part serial numbers, cavity numbers, and inspection temperature (20 ± 2 °C)
- Check that profile of a surface is reported as a total band, not a single max deviation
- Confirm MMC bonus tolerance is calculated and shown separately from the base tolerance
- Review measurement uncertainty against each tolerance; require guard banding where uncertainty exceeds 10% of tolerance
- Cross-check the number of reported characteristics against the ballooned drawing
- Request raw point data for any result within 20% of the tolerance limit
What to Do When a Report Fails
A failing characteristic is not automatically a rejected lot. First determine whether the failure is real or an artifact of setup: re-inspect the part with the datum scheme corrected, and if the value moves by more than 30% of the tolerance, the original setup was likely wrong. For marginal failures (within 10–15% over tolerance) on non-critical features, a deviation concession may be appropriate if the function is unaffected, but document it against the drawing and get engineering sign-off.
For repeated failures on the same characteristic across lots, the issue is usually process capability rather than inspection. Ask for a 30-piece capability study (Cpk) on that feature; a Cpk below 1.33 on a casting characteristic means the process, not the CMM, needs attention. Keep the CMM report, the raw data, and the concession record together so the next lot's report can be compared against a known baseline.
Frequently Asked Questions
Should I accept a CMM report that uses best-fit alignment instead of the drawing's datum scheme?
No, not for acceptance. Best-fit alignment distributes error across all features and can make a warped or shifted casting appear conforming. Ask for a re-inspection using datum-only alignment that matches the drawing's A-B-C reference frame, and require the alignment method to be stated in the report header.
The report shows profile of a surface within tolerance, but the part doesn't fit the mating assembly. What went wrong?
Most likely the profile was reported as a maximum deviation rather than a total band, or the datum scheme differs from the assembly's functional datums. Request the raw point data and the min/max deviations on both sides of the surface, and confirm the datum targets match the drawing.
How much measurement uncertainty is acceptable on a casting CMM report?
As a rule, uncertainty should be 10% or less of the tolerance being verified. Above that, require the supplier to apply guard banding, accepting only parts inside roughly 80–90% of the tolerance, so marginal parts are not passed on the strength of measurement noise.
Looking for a reliable casting supplier? Request a quote from Intercontinental Casting — our engineering team replies within one business day.