
Auditing a Chinese Foundry: A 40-Point Walkthrough
Publication Date : 2026-11-07 03:10:43
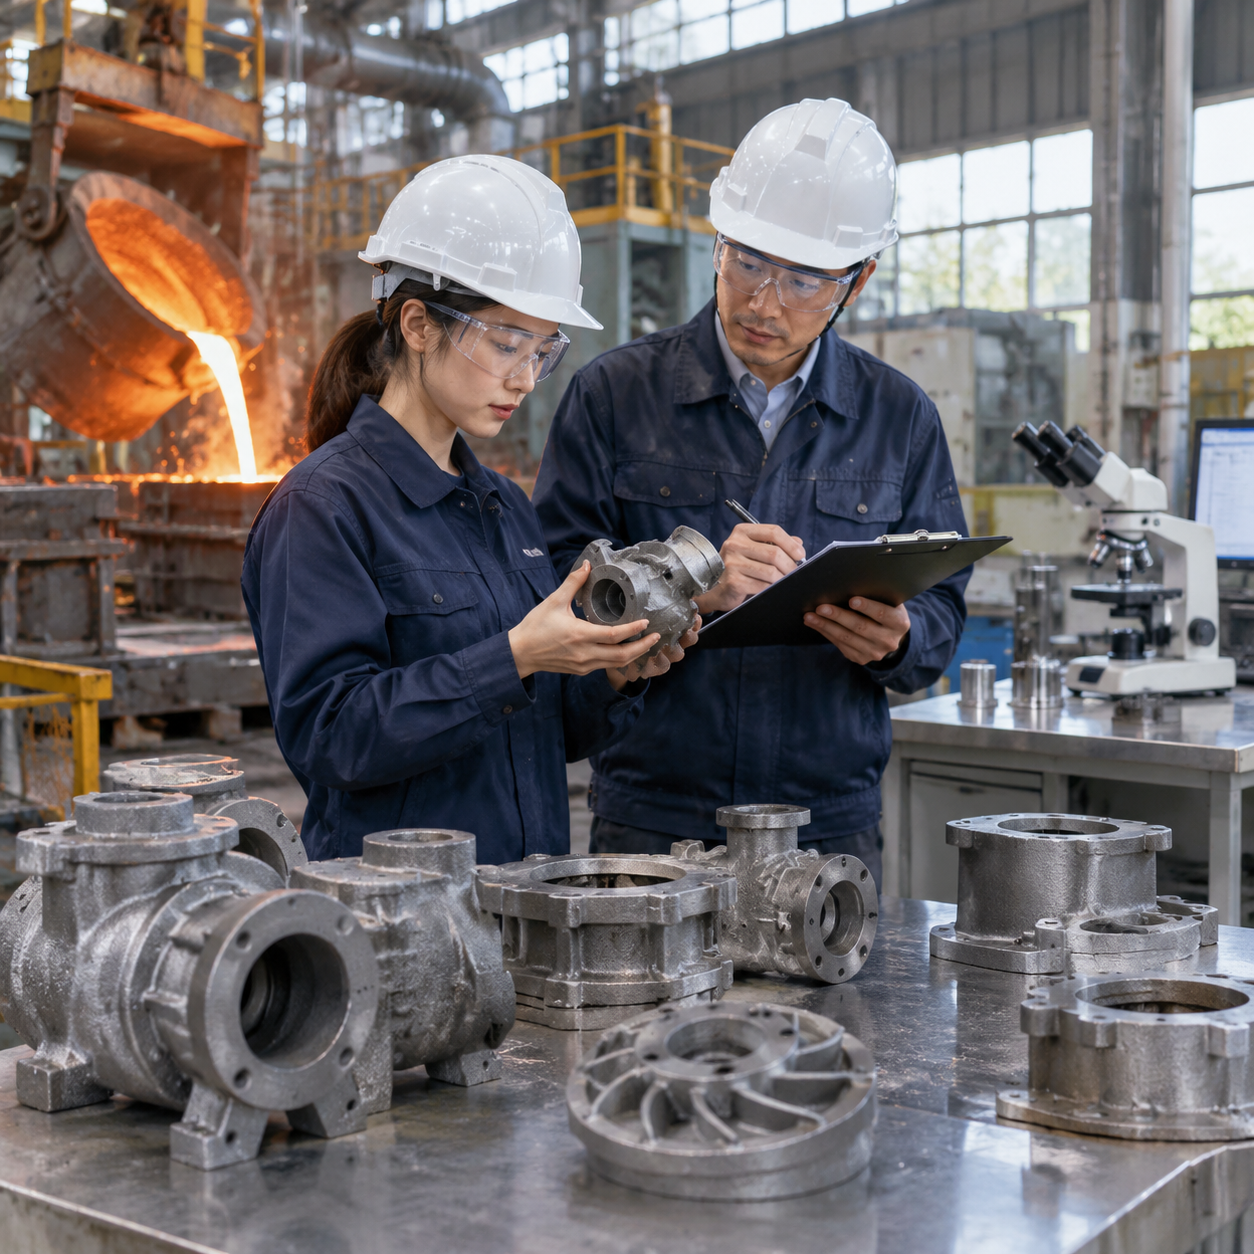
A practical 40-point audit sequence for overseas buyers visiting a Chinese foundry, covering melting, molding, the QC lab, traceability and calibration, with scoring guidance and realistic acceptance thresholds.
How to Structure the 40-Point Audit
Split the 40 points across four zones so the walkthrough follows the metal: melting and charge control (12 points), molding and core making (10 points), QC lab and dimensional inspection (10 points), and traceability plus calibration (8 points). Score each point 0 (absent), 1 (present but undocumented), or 2 (documented and verified on the floor). A 40-point audit therefore maxes at 80. In our experience buyers should treat 64/80 (80%) as the floor for a first order and 72/80 (90%) before committing to a multi-year program; anything below 48/80 means the foundry is running on operator habit rather than a system.
Walk the floor in process order and ask to see the record for the heat you just watched poured, not a sample file from last month. Time-box the visit: 90 minutes on melting and molding, 60 minutes in the lab, 30 minutes on records. If the plant manager cannot produce the paperwork for a specific heat within 10 minutes, deduct the documentation point regardless of what the file cabinet contains.
Melting and Molding: The 22 Floor Checks
In melting, verify charge materials are segregated by grade with visible tagging; scrap should be clean, painted scrap rejected, and pig iron or returns weighed per heat rather than shovel-counted. Ask for the furnace log: heat number, charge weight, chemistry target, and tap temperature. For grey and ductile iron, tap temperatures commonly run 1,400–1,480°C; for carbon steel, 1,600–1,650°C. Confirm a spectrograph result exists for each heat and that the carbon equivalent is recorded, not just individual elements. Check inoculation practice for ductile iron: magnesium treatment method, wire or sandwich, and a record of the Mg residual (typically 0.03–0.06%) plus a nodularity check.
In molding, look at pattern condition and storage, sand system control (green sand compactability is commonly held around 35–45%, with moisture roughly 3.0–3.8% for iron), and core venting. Ask how mold hardness or compaction is checked and see the gauge. Verify pouring temperature is recorded per ladle and that a pyrometer is used, not judged by eye. On the shakeout and cleaning line, confirm that heat numbers are transferred onto castings or their tubs before shot blasting removes any marking.
- Charge materials tagged by grade and supplier; painted or oily scrap segregated
- Furnace log per heat: heat number, charge weight, tap temperature, chemistry
- Spectrograph result on file for every heat, carbon equivalent calculated
- Ductile iron: Mg residual and nodularity recorded per treatment
- Pouring temperature recorded per ladle with a calibrated pyrometer
- Green sand: compactability, moisture and permeability tested each shift
- Pattern storage dry, identified, and inspected for wear before each run
- Core vents clear; core wash and drying records available
- Mold hardness or compaction checked with a gauge, not by eye
- Heat number transferred to castings or tubs before shot blasting
- Ladle and refractory condition checked; lining life logged
- First-article casting from each pattern retained as a reference sample
QC Lab, Traceability and Calibration: The 18 Desk Checks
The lab is where most audits are won or lost, because it is easy to fake and easy to verify. Confirm the spectrometer is calibrated with certified reference materials and that the calibration log is dated within the last shift or day, depending on plant practice. Mechanical testing should include tensile and hardness on a defined frequency, commonly one tensile bar per heat or per shift for critical parts; ask for the frequency written in the control plan and then count the results against the heats poured last month. For dimensional inspection, check that CMM programs are revision-controlled and match the drawing revision the buyer supplied.
Traceability is a paper exercise until you test it: pick a finished, packed casting and ask the team to walk it back to heat number, pour time, molding line, and incoming charge lot. That round trip should take under 15 minutes and end with a name. For calibration, list every gauge used in the checks above, then verify each has a sticker, a due date, and a certificate traceable to a national standard; a plant with 30 gauges and 3 overdue is a management problem, not a paperwork problem.
Turning the Walkthrough Into a Score
Score on the floor, not in the meeting room, and photograph the evidence for each 2. Weight the four zones as in the chart above so a strong lab cannot mask a weak melt. Any zero on a critical point, such as no chemistry record per heat, no calibration on the spectrometer, or no traceability from finished part to heat, should cap the total at 60/80 regardless of other scores. Share the scored sheet with the foundry the same day and ask for a written corrective-action list with owners and dates; a foundry that returns it within a week is signalling how it will handle quality escapes.
Re-audit the failed points at the next order, not the next year, and keep the same 40-point sheet so scores are comparable visit to visit. Buyers running three or more suppliers should standardise the sheet across all of them; a 10-point gap between two foundries on the same sheet is a more useful signal than any brochure.
Frequently Asked Questions
How long should a foundry audit take, and who should attend?
Plan a full day: about 90 minutes on melting and molding, 60 minutes in the lab, 30 minutes on records, and the rest for the closing meeting. Bring someone who can read a chemistry certificate and a drawing, plus an interpreter if the QC staff do not work in English. Do not accept a slide presentation in place of the floor walk.
What score should a foundry reach before I place a first order?
On the 80-point scale described here, treat 64/80 (80%) as the minimum for a first order and 72/80 (90%) before a long-term program. A score below 48/80 means the process depends on individual operators rather than documented control, and any zero on chemistry records, spectrometer calibration, or heat traceability should cap the total at 60/80.
Can I audit a foundry remotely?
Partially. You can review certificates, control plans, calibration lists, and photos or video of the melt and lab, but charge segregation, sand control, pattern condition and the traceability round trip need someone on the floor. A practical compromise is a remote document review followed by a one-day on-site visit before the first production run, then annual on-site re-audits.
Looking for a reliable casting supplier? Request a quote from Intercontinental Casting — our engineering team replies within one business day.